


Complete Lifting Solution for a Quarry and Stone Processing Plant
SEVENCRANE recently secured a comprehensive lifting equipment project for a leading quarry and natural travertine furniture manufacturer in Armenia. The order included a 30-ton European double girder gantry crane, two European single girder overhead cranes, two BZ pillar jib cranes, and two stone clamps. Providing a complete material handling solution for stone processing and manufacturing operations. The project was delivered under EXW terms with a production period of 30 working days. Meeting the customer's strict delivery requirements.
The customer is the owner of a quarry and furniture manufacturing company specializing in natural travertine products. Their production process involves transporting large stone blocks from the quarry, moving them through cutting and processing lines. And finally handling finished stone products inside different workshops. To improve production efficiency while reducing manual handling, the customer required multiple customized lifting systems for different working areas.
The largest piece of equipment supplied was an NMHII European double girder gantry crane with a 30-ton lifting capacity, 6.35-meter lifting height, and a span configuration of 4.5 + 10 + 4.5 meters. The crane was equipped with a remote control and pendant control system, together with 75 meters of P43 rail and a complete cable reel system. Since the gantry crane would be used to lift heavy stone blocks in the quarry, one important requirement was that the clear distance between the gantry legs had to allow 4 × 4-meter stone blocks to pass freely from both sides. Our engineering team optimized the gantry structure to satisfy this requirement without compromising lifting stability.
To improve operational safety, the customer also requested that the cable reel be installed on the outside of the gantry leg instead of the standard position. This customized arrangement prevents accidental contact between the cable reel and large stone blocks during lifting operations. Reducing the risk of equipment damage and ensuring safer daily production.
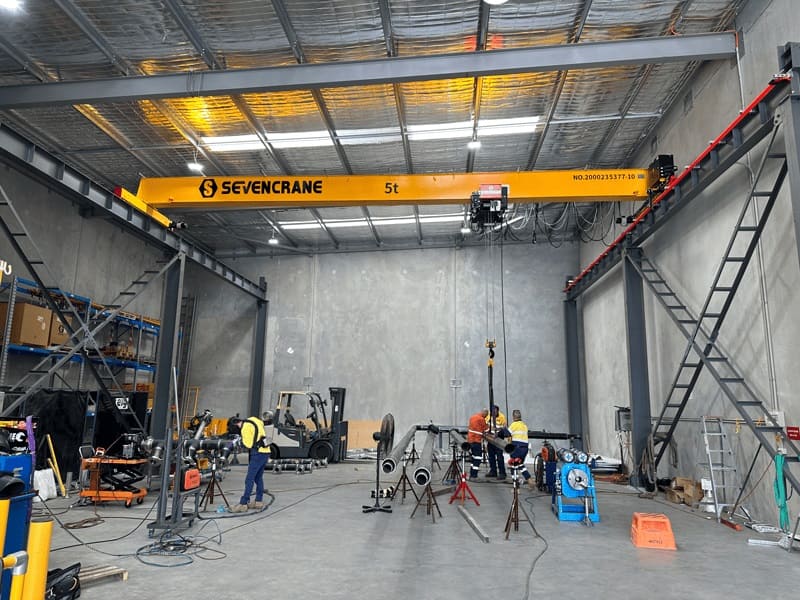
In addition to the gantry crane, SEVENCRANE supplied two SNHD European single girder overhead cranes. Each with a 5-ton lifting capacity. The cranes were installed in two separate workshops with different building dimensions. One crane featured a 16.37-meter span, while the other had a 14.6-meter span. Both cranes were supplied with supporting runway beams, P24 rails, and conductor busbar systems. Since the available space between the runway beam and the workshop roof was very limited, our engineering team carefully reviewed the customer's drawings and optimized the crane dimensions to maximize lifting height while maintaining safe installation clearances.
The project also included two manual rotation BZ pillar jib cranes, each with a 1.5-ton lifting capacity. As well as two stone clamps specially designed for handling stone slabs and blocks. These jib cranes provide flexible lifting assistance for loading, positioning, and rotating stone materials during processing, significantly improving workplace efficiency.
This project developed gradually through continuous communication. Initially, the customer only planned to purchase one gantry crane and one overhead crane. During discussions, they explained that if the price was competitive, they would consider purchasing additional equipment. After reviewing our first quotation, they expanded the project by adding another overhead crane and two jib cranes.

To help the customer evaluate our solution, SEVENCRANE shared several successful reference projects in similar stone processing applications. The customer appreciated our experience and product quality. But also explained that they had received quotations from suppliers in Iran, Türkiye, and China. Their main concerns were delivery time and overall project cost.
During negotiations, the customer revealed that another Chinese supplier could deliver the equipment by the end of the following month and requested additional price discussions. After carefully evaluating the project, SEVENCRANE offered a competitive discount while maintaining the promised 30-working-day delivery schedule, which became the deciding factor in winning the order.
Every piece of equipment underwent strict quality inspections, electrical testing, dimensional verification, and load testing before shipment. Our engineering team also prepared detailed technical documents to support installation and commissioning after delivery.
This successful project demonstrates SEVENCRANE's capability to provide complete, customized lifting solutions for demanding industries such as quarrying and stone processing. By combining professional engineering, competitive pricing, fast delivery, and reliable product quality, we continue to help customers worldwide improve productivity. And build long-term partnerships based on trust and performance.


